How Is TR90 & TPEE Dual-Material Molding Done in Kids Sunglasses, and What Quality Factors Does It Affect?
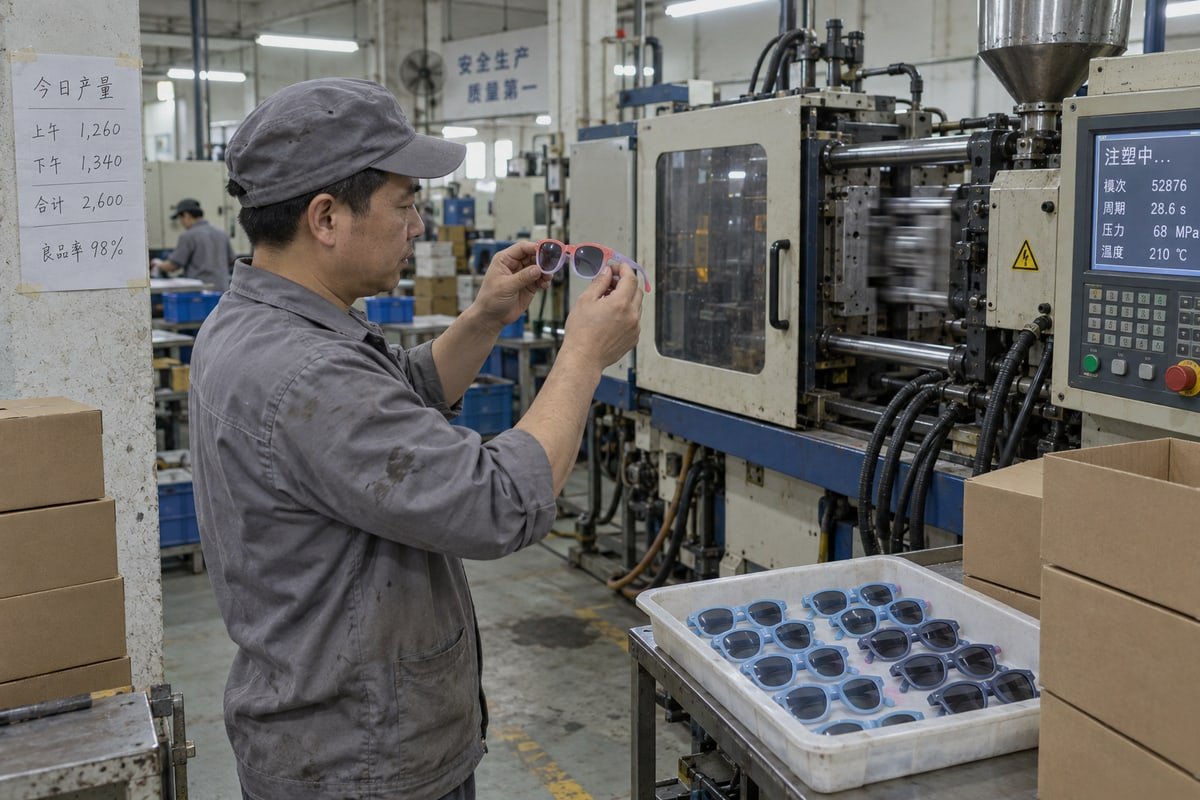
TR90 and TPEE dual-material molding in kids sunglasses looks simple until a bonded temple peels in a child’s hands CE documentation 1. On our Taizhou line, we learned that lesson early.
TR90 and TPEE dual-material molding uses two-shot injection: a rigid TR90 frame or temple core is molded first, then soft TPEE is overmolded onto nose pads, temple tips, and grip zones. It affects bond strength, fit, weight, flexibility, impact resistance, surface finish, and child safety.
Below, I will walk through how the process works on a real production floor. Then I will show you which quality factors it touches, why supplier capability matters, and how to audit the frames you already buy.
How does the TR90 and TPEE dual-material molding process actually work in kids sunglasses?
Last spring, a QC inspector on our line pulled a pink frame because the TPEE tip lifted under a thumbnail. That one part taught us more than any spec sheet.
The process runs in two shots. First, pre-dried TR90 pellets are injected into a mold to form the frame or temple core. Then the part moves to a second cavity, where heated TPEE is overmolded onto grooves and anchor holes, fusing at the interface as it cools.
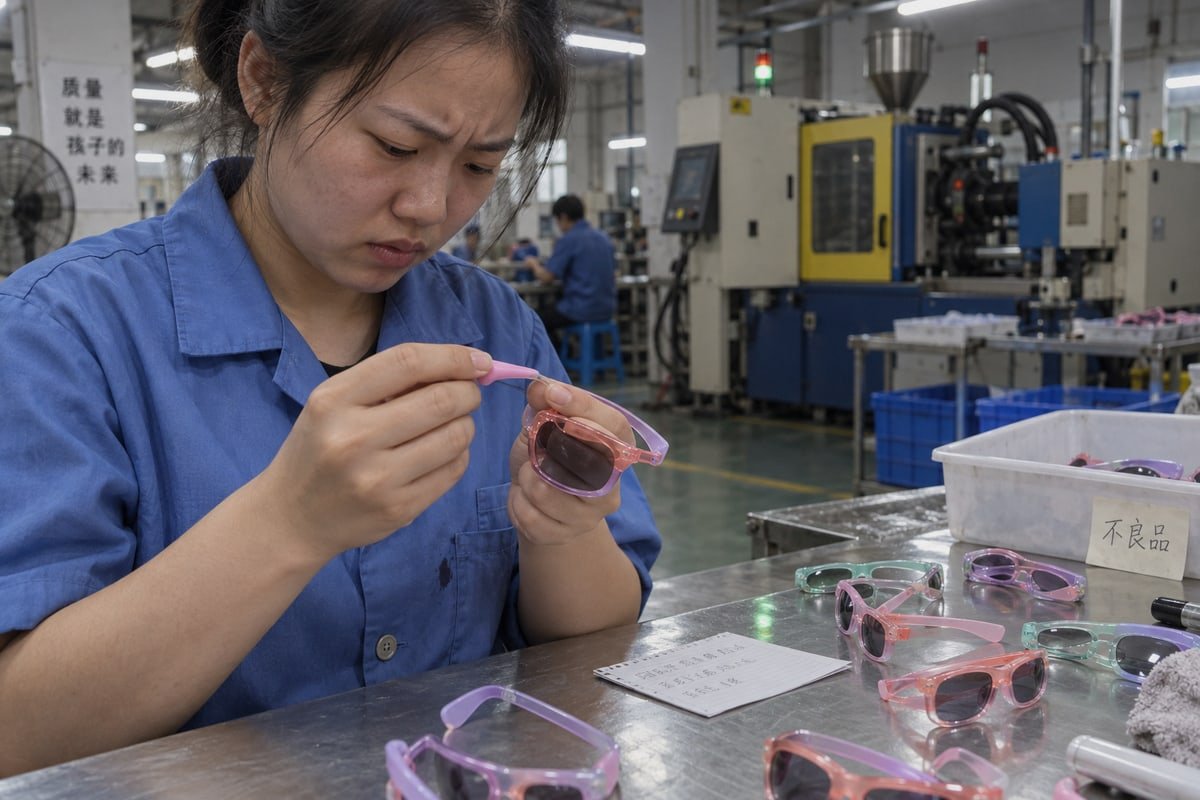
People often picture the two materials being glued or snapped together. That is not how it works. Two-shot injection molding is one continuous cycle on one machine, and the bond forms inside the mold, not on a bench.
Step by step on the production line
- Drying. TR90 is a Grilamid polyamide. It absorbs moisture from the air 2, so we pre-dry the pellets before every run. Wet pellets create bubbles and warping. Bio-based TR90 made from castor oil is even more hygroscopic. It needs vacuum-drying protocols, or steam forms at the bonding interface and shows up as silver streaks.
- First shot. The dried TR90 is melted and injected under pressure into the frame or temple cavity. A typical TR90 injection cycle 3 runs about 35 to 45 seconds. This shot sets the shape, the hinge seats, and the lens groove.
- Transfer. The still-warm TR90 core rotates or is moved to a second cavity. Timing here matters. If the core cools too much, the second material will not fuse to it.
- Second shot. TPEE is injected onto the exposed zones. The incoming melt must slightly re-melt the TR90 surface. That surface softening allows molecular diffusion 4 across the interface. This is why mold temperature control is the single most critical variable in the overmolding process.
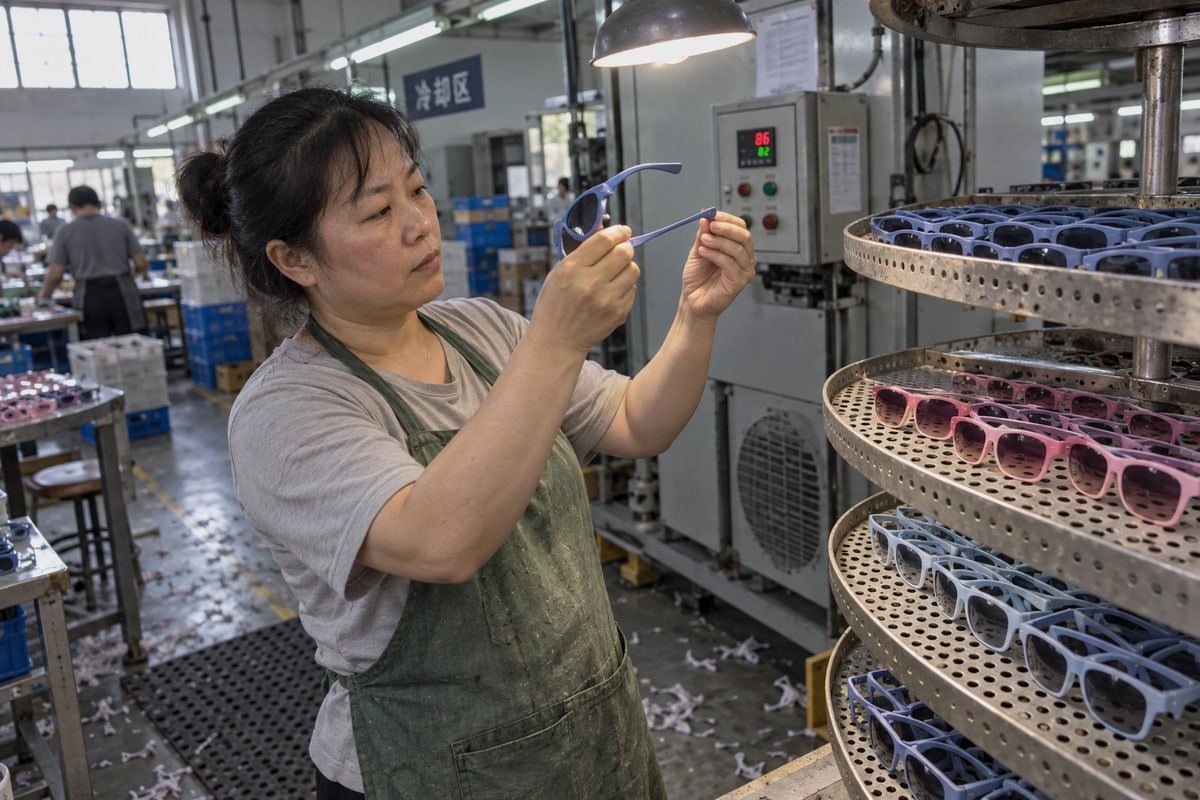
- Cooling. The two materials shrink at different rates. If cooling is not balanced across both shots, internal stress builds, and the frame can warp or "smile" upward at the temple ends.
- Trimming and inspection. Gates are trimmed, and the part is checked for flash, mold lines, and lift at the edge of the TPEE.
Where the two materials can fail each other
| Stage | What should happen | What goes wrong when it does not |
|---|---|---|
| Drying | Moisture removed from TR90 pellets | Bubbles, silver streaks, weak interface |
| First shot | Clean, complete TR90 core with anchor features | Short shots, sink marks, missing grooves |
| Second shot | TPEE re-melts TR90 skin and fuses | Cold bond, peel under thumbnail pressure |
| Cooling | Balanced shrinkage across both materials | Warped temples, gapped lenses |
In our workshop, we treat the second shot as the pass-or-fail moment. Everything before it is preparation. Everything after it is verification. TR90 and TPEE dual-material molding rewards discipline more than clever design.
What quality factors should I check to ensure the two materials bond safely and durably?
Every time we thicken a TPEE layer, we weigh it against bond area and cooling balance. Softer feel is easy. Softer feel that stays attached for two summers is harder.
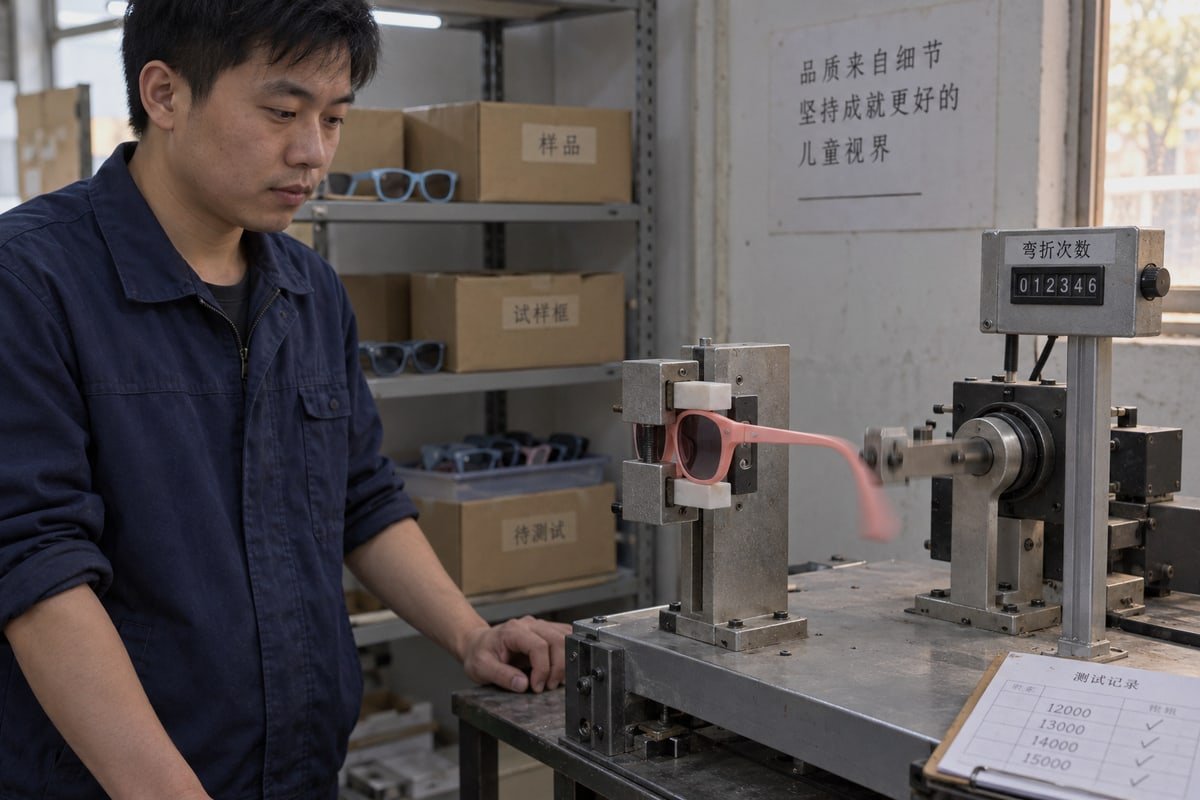
Check interfacial adhesion with a peel and twist test, look for mechanical anchors in the TR90 core, confirm bonding-grade resin pairing, inspect for warpage and silver streaks, verify frame weight under about 20 grams, and test bend recovery, hinge stability, and lens retention after repeated flexing.
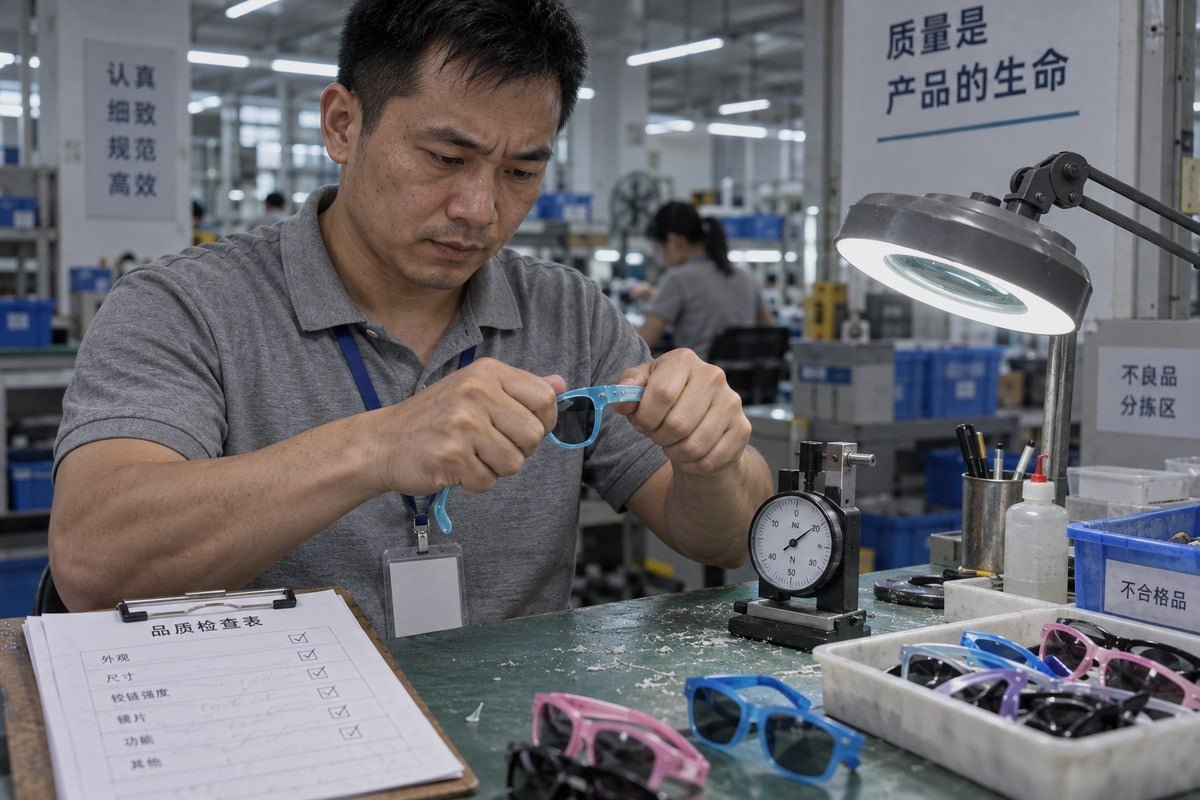
A bond you cannot see is still a bond you can test. Our QC team uses a short list of hands-on checks, and I recommend buyers use the same ones when a sample arrives.
Bond strength at the interface
TR90 is a polyamide. TPEE is a polyester elastomer. The two do not bond naturally. Good factories solve this in three ways, and the best use all three at once.
- Bonding-grade resins. Specific TPEE grades are formulated to adhere to polyamide. A generic TPEE will feel identical in the hand but peel far sooner.
- Mechanical interlocks. Dovetail grooves, undercuts, or through-holes in the TR90 skeleton give the TPEE a physical anchor. If the chemical bond weakens over time, the shape still holds the layer in place.
- Surface preparation. Chemical primers are one option. Laser-induced surface texturing on the TR90 substrate is an emerging alternative. It cuts micro-scale anchors into the surface and raises peel strength without adhesive chemistry.
Ask your supplier which of these three they use. A vague answer is a warning sign.
Geometry, weight, and warpage
Differential shrinkage is the quiet enemy. TR90 and TPEE cool and contract at different rates. Poor balance leaves internal stress in the temple. The frame may look fine in the box and twist a month later. I check every new tool by laying frames flat and looking for temple lift.
Weight matters too. Sourcing guides often suggest keeping kids' frames under about 20 grams. It is a practical target, not a formal standard, but a heavy frame slides down small noses no matter how soft the pads are.
Finish and long-term feel
| Quality factor | How dual molding affects it | Quick check |
|---|---|---|
| Interfacial adhesion | Decided by resin pairing, mold temperature, anchors | Thumbnail peel at TPEE edge, twist temple 90 degrees |
| Flexural strength | TR90 core carries load; TPEE dampens stress | Bend temple around fingers, confirm full recovery |
| Impact resistance | TPEE at hinge and bridge absorbs shock | Drop test on hard floor from table height |
| Soft-touch finish | Gate control, mold polish, TPEE grade | Look for flash, rough texture, visible mold lines |
| Surface stability | Oleophobic additives resist sunscreen and skin oils | Rub with sunscreen, wipe, check for tackiness |
| Lens retention | Balanced cooling keeps lens groove true | Press lens center, listen for rattle |
Two details deserve extra attention. First, some newer TPEE formulations add oleophobic additives. Skin oil, sunscreen, and UV exposure can turn plain elastomers sticky over time. Second, TPEE placed at the hinge and bridge acts as a vibration damper. It protects the stiffer TR90 from snap failures in cold weather, which matters for buyers in northern Europe and Japan.
Why do I need to verify a supplier's dual-material molding capability before placing a bulk order?
A procurement manager from Australia once asked why the molding method mattered if the sample felt fine. I showed her two parts after repeated bending.
Verify capability because dual-material molding demands tighter process control than single-shot frames. A supplier without proper two-shot tooling, material compatibility knowledge, and repeatable cycle control can pass a sample yet ship delaminating, warped, or inconsistent frames in bulk, exposing your brand to returns and child-safety risk.
Before we talk about capability, it helps to see why buyers choose the dual design in the first place. Here is how the three construction options compare.
| Construction | Best age fit | Strengths | Weak points |
|---|---|---|---|
| TR90-only | Roughly 6 to 12+ | Strong shape memory, high impact resistance, crisp look | Harder contact points, less grip for small heads |
| TPEE-only | Roughly 0 to 3 or 0 to 5 | Very soft, chew-resistant, forgiving for toddlers | Lower structural stability, lenses can shift |
| TR90 core + TPEE overmold | Roughly 3 to 12+ | Light, springy, soft where it touches skin | Needs strict process control and better tooling |
The objections I hear, and how I answer them
"TR90 alone is the better all-round kids material." For older children, TR90 does give stronger shape recovery and confidence in daily use. I agree. But a school-age child still has ears and a nose. Soft TPEE tips and pads cut pressure points and slipping during sport. The core stays TR90. Only the touchpoints change.
"TPEE alone is safer for very young children." For a teething toddler, a fully soft frame is often the right call, and we make plenty of them. The trade-off is lens security. Once a child is running, jumping, and pulling glasses off by one temple, a TR90 skeleton holds the lens groove true while TPEE keeps the feel gentle.
"Dual-material molding costs more." It does. Tooling is more complex and the cycle is longer. TPEE-only products are usually cheaper, and TR90 is positioned as the higher-end option. The dual design is how we balance price and performance in one frame. The real cost risk is not the unit price. It is a bulk shipment that fails after the sample passed.
What capability actually looks like
A factory that can run TR90 and TPEE dual-material molding well should be able to show you:
- Two-shot or rotary-platen machines, not a single-shot press plus manual assembly.
- Dryer records for TR90, including vacuum drying if bio-based grades are used.
- Material data sheets proving material compatibility between the chosen TR90 and TPEE grades.
- Tool drawings showing anchor features in the TR90 core.
- A repeatability record, meaning production units that match the approved sample in weight, color, and bond.
After fifteen years in eyewear, our engineers hold about 800 existing styles that already run stable on our tools. For a new brand, that means you can test the market with a proven dual-material frame before committing to your own mold. Custom colors, logos, lens tints, and packaging then sit on top of a process we already trust.
How can I tell if my current supplier's dual-injection molding meets safety standards for children?
One lesson stuck with me after fifteen years in eyewear: a supplier's paperwork never tells you what a child's mouth or a hot car will.
Ask for material data sheets confirming BPA-free, hypoallergenic TR90 and TPEE grades, request lens UV400 and CE documentation, inspect edges and mold lines for sharpness, run peel, bite, and bend checks on production units, and compare bulk shipments against your approved golden sample for consistency.
Both TR90 and TPEE are inherently BPA-free and hypoallergenic when genuine grades are used. That is a good start. It is not the finish line. Safety in a child's frame lives in the details of how those materials were molded, finished, and assembled.
Start with the documents
Ask for the resin supplier's data sheet for each material. Confirm the grade names match what was quoted. Fake or recycled "TR90" is a known issue in the market, and it will not behave like true Grilamid polyamide under bending or heat. For lenses, request the UV400 report 5 and the CE documentation that supports the marking on the lens sticker. Match the report to the tint and polarization you actually ordered.
Then test the frames yourself
| Check | Pass looks like | Red flag |
|---|---|---|
| Edge inspection | Smooth, rounded edges; no sharp gate remnants | Raised flash, sharp mold lines near the eye |
| Peel and bite test | TPEE stays fixed under thumbnail and firm bite | Edge lifts, tears, or shows adhesive residue |
| Bend recovery | Temple returns flat after full wrap around fingers | Set bend, whitening, or crack at the TPEE edge |
| Hinge cycle | Even tension after many open-close cycles | Loosening, rattle, or misalignment |
| Lens retention | Lens stays seated under center press | Gap, rotation, or click sound |
| Sunscreen rub | Surface wipes clean and stays dry | Tacky or cloudy TPEE |
| Heat exposure | Frame keeps shape after a warm car test | Temple warps or lens pops |
These checks take under ten minutes per sample. They catch most of the failures that upset parents and trigger returns.
Look at consistency, not just one unit
A single perfect sample proves the tool can work. It does not prove the factory runs it the same way every shift. Weigh ten frames from a bulk carton. They should sit within a tight band of each other. Compare color between the translucent front and the matte temple across the carton. Check that the soft-touch finish feels the same on every temple tip. Our 5S-managed workshop with around 120 workers exists for exactly this reason. Consistency is a habit, not a feature.
Match the frame to the child
Finally, judge safety by age. Skin-friendly materials matter most for toddlers who chew. Impact resistance and lens retention matter most for school-age children who play sport. If a supplier sells one construction for every age, ask why. We ship to brands in more than twenty countries, and the good ones always ask us about age range first.
Conclusion
Dual-material molding is where comfort, safety, and durability are decided. Choose a partner who controls the bond, proves it in bulk, and stands behind every child-sized frame.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
Footnotes
1. Official European Commission requirements for product compliance, marking, and technical documentation. ↩︎
2. Authoritative Wikipedia entry defining the physical property of materials absorbing moisture from the atmosphere. ↩︎
3. Provides a detailed overview of the injection molding stages and cycle parameters. ↩︎
4. Scientific explanation of the molecular movement required for chemical bonding between different polymer materials. ↩︎
5. Authoritative health guidelines regarding ultraviolet radiation protection and sunglasses safety standards. ↩︎
More Articles You Might Like
Looking for a Reliable Kids Eyewear Partner?
Explore 800+ ready styles and full OEM/ODM support tailored to your brand.
Get in Touch English
 Español de México
 Deutsch
 Français
 日本語
 العربية
 Português do Brasil